Choosing the right Pouch Cell Trimming Machine can influence cell quality, production stability, and long-term operating costs. The decision involves more than cutting speed. It requires attention to edge accuracy, burr control, dust management, fixture design, and operator safety.
Battery manufacturing expert Dr. Shirley Meng has said, “Manufacturing consistency turns promising chemistry into a dependable product.” This principle matters during pouch cell trimming. A clean, repeatable cut protects the aluminum-plastic pouch and supports reliable downstream sealing. Even a small edge defect may cause sealing problems, material waste, or later quality concerns.
That sounds obvious. It is not.
A suitable Pouch Cell Trimming Machine should match the cell dimensions, material structure, and expected production volume. Buyers should examine trimming tolerance, blade or punch durability, changeover time, and vision inspection options. Automatic positioning can reduce operator variation. Closed dust collection can protect nearby equipment and improve the working environment.
Faster is not always better.
Some machines achieve impressive cycle times but create excessive heat, vibration, or maintenance demands. A slower system may deliver better consistency in real production. Ask suppliers for sample-trimming results, edge photographs, maintenance records, and measurable acceptance standards. Factory trials are valuable because brochures rarely reveal every weakness.
This guide examines how to compare machine construction, control systems, safety features, service support, and total ownership costs. It also considers an uncomfortable question: are you choosing for today’s output, or for tomorrow’s product changes? A thoughtful answer can prevent an expensive and avoidable equipment decision.
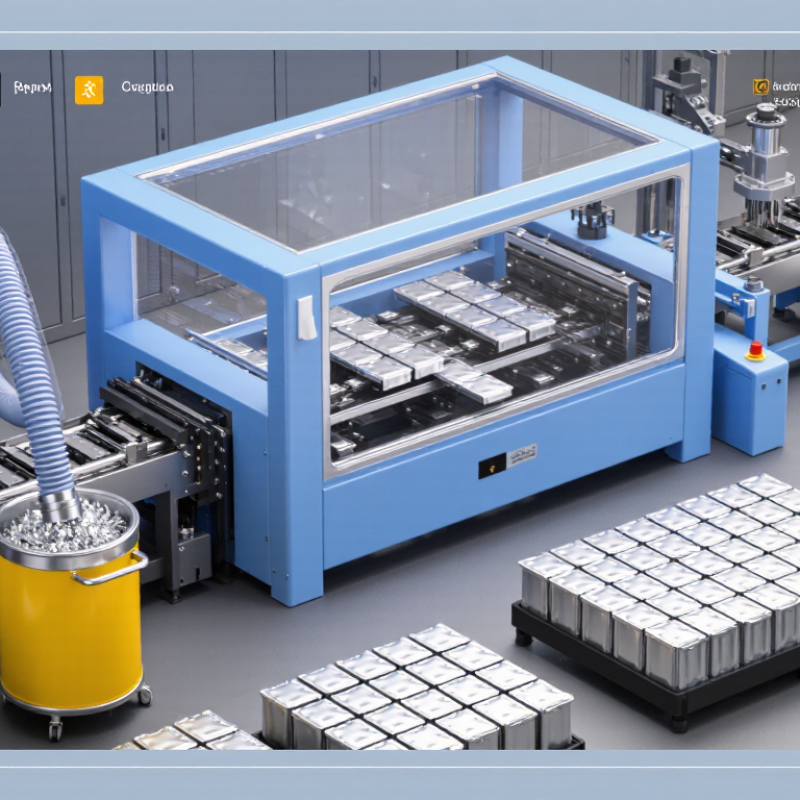
A pouch cell trimming machine removes excess aluminum-plastic film from a sealed battery cell. It cuts the pouch edge to a controlled shape without damaging the electrode stack or sealing area. In production, this process follows forming and sealing, where uneven edges can affect later assembly.
Why does it matter? Accurate trimming improves cell dimensions, stacking consistency, and handling stability. A clean edge also reduces loose film, sharp corners, and possible interference during module assembly. Small defects may seem harmless. They can become serious alignment problems later. From practical production experience, trimming quality depends on blade sharpness, clamping pressure, positioning accuracy, and material variation. No machine performs perfectly under every condition, so sample testing remains necessary. This point is sometimes underestimated.
Tips: Check edge quality under strong lighting. Measure trimmed width at several points. Inspect for burrs, wrinkles, exposed metal, and seal damage. Ask for trial samples using your actual pouch material. Also review adjustment access, sensor reliability, cleaning time, and maintenance records. A machine with impressive speed may still create costly rework. Operators should record settings and inspect the first pieces of each batch. That simple habit often reveals drift early. Choose equipment with stable control, clear safety protection, and responsive technical support. The best choice is not always the fastest machine. It is the one that repeatedly produces clean, consistent edges with manageable operating effort.
Before comparing machines, define the pouch cell requirements precisely. Record cell length, width, thickness, aluminum-plastic film type, and acceptable dimensional tolerance. Include the tab position and sealing area. A few millimeters can change the fixture design. Do not rely only on supplier drawings. Measure actual production samples, because material shrinkage and sealing variation may appear later.
Define the trimming result next. Specify the cutting path, edge tolerance, burr limit, dust control, and maximum deformation. Decide whether the machine must process one cell or several cells per cycle. Production speed matters, but stable quality matters more. Review changeover time, fixture replacement, operator access, and data traceability. Automation can help, though it may add maintenance points. I have seen specifications become too ambitious. A simpler system sometimes performs better.
Tips:
Prepare a requirement sheet with three levels: essential, preferred, and optional. Test samples with different thicknesses and sealing conditions. Ask for measurable acceptance criteria, not vague claims such as “high precision.” Check inspection records, trial-cut results, and service response procedures. Leave room for adjustments after pilot testing. The first specification is rarely perfect. That is normal. Revisit it after observing cut edges under magnification and checking cells after thermal cycling.
Machine structure directly affects trimming stability, maintenance, and operator safety. A rigid welded frame reduces vibration during high-speed cutting. Check whether the blade holder supports quick adjustment and secure locking. Inspect access panels, guarding, and waste collection before making a decision. These details often matter more than an impressive production speed. In practical trials, uneven clamping can create small burrs along pouch edges. That problem may appear only after several hours of operation.
Cutting accuracy should be tested with your actual pouch dimensions and materials. Ask for repeated samples, not one perfect piece. Measure edge position, burr size, and corner consistency with calibrated tools. Vision sensors can correct positioning, but they cannot fix poor mechanical alignment. Automation should connect feeding, trimming, inspection, and rejection without frequent manual intervention. Useful systems also record alarms, batch data, and blade replacement intervals. However, excessive automation can complicate troubleshooting. This is an area where I would still review the workflow carefully.
Tips: Compare three sample runs under identical settings. Watch the operator, not only the machine. Check changeover time, noise, cleaning effort, and access to spare blades. Request training records and maintenance procedures. A lower initial price may become expensive when adjustment takes too long. Test the machine with slight material variation, because perfect laboratory samples can create false confidence.
How to Evaluate Safety, Compatibility, Maintenance, and Production Capacity
Pouch cell trimming now demands more than a sharp blade and fast cycle time. The International Energy Agency reported that global electric-vehicle battery demand exceeded 750 GWh in 2023. This growth raises pressure on every forming and finishing process. A suitable machine should include guarded cutting zones, interlocked doors, emergency stops, dust extraction, and controlled access to moving parts. Safety functions should align with recognized machinery standards, such as ISO 13849, and battery safety requirements should be reviewed with the final cell design.
Compatibility starts with dimensions. Check pouch length, width, thickness, tab position, sealing margin, and allowable burr size. Ask for trials using your actual aluminum-plastic laminate and electrode stack. A machine may trim one format well, then struggle with another. Small deviations can cause seal damage or expose conductive layers. That is expensive.
Maintenance deserves equal attention. Select modular blades, visible adjustment points, tool-free cleaning areas, and recorded replacement intervals. A spreadsheet can still lie. Confirm mean time to repair through service records, not promises. For capacity, compare proven cycle time, first-pass yield, changeover duration, uptime, and operator loading. Theoretical output is rarely real output. Review at least one month of production data, including stoppages and rejected cells, before approving the purchase.
Selecting the best pouch cell trimming machine starts with the application, not the catalogue. Cell size, film type, sealing structure, edge geometry, and daily output should guide the specification. The IEA’s Global EV Outlook 2024 reported that electric vehicle battery demand exceeded 750 GWh in 2023, rising by about 40% in one year. This growth increases pressure on manufacturers to achieve stable trimming quality at higher production speeds.
For high-volume automotive cells, choose equipment with controlled cutting force, automatic alignment, dust extraction, and real-time inspection. A clean edge matters because loose film particles can affect sealing and downstream assembly. For laboratory or pilot production, flexible tooling and fast recipe changes may be more valuable than maximum speed. Check whether the machine handles your actual pouch dimensions, not only standard samples. Small differences can expose weaknesses.
Measure cycle time using production conditions. Include loading, inspection, tool changes, and stoppages. A quoted speed may look impressive. It may not reflect real output. Review repeatability data, reject rates, safety functions, and maintenance access. The U.S. Department of Energy’s Battery Manufacturing R&D Roadmap emphasizes process control, quality consistency, and scalable manufacturing as key development needs. I would also request trial runs with your own cells. A perfect specification sheet is not enough. Operators often reveal practical problems that testing documents miss.
| Selection Dimension | Manual or Benchtop Trimming | Semi-Automatic Trimming | Servo-Controlled Automatic Trimming | Inline High-Throughput Trimming |
|---|---|---|---|---|
| Typical application | Laboratory development, sample preparation, pilot trials, and low-volume production. | Small-batch production and manufacturing lines requiring operator loading with automated cutting. | Medium- to high-volume production with repeatable positioning and recipe-based operation. | Continuous mass production integrated with forming, sealing, inspection, and packaging equipment. |
| Typical output rate | Approximately 20–80 cells per hour, depending on loading and inspection time. | Approximately 120–300 cells per hour. | Approximately 300–900 cells per hour. | Approximately 900–2,400 cells per hour, depending on cell size, trim path, and line balance. |
| Operator involvement | Manual loading, alignment, cutting, and part removal. | Manual loading and unloading; cutting cycle and clamping are automated. | Operator loads material or uses an automatic feeder; motion, clamping, and cutting are recipe-controlled. | Minimal direct handling; transfer, positioning, cutting, and discharge are coordinated with the production line. |
| Suitable pouch-cell formats | Best for frequent format changes and experimental cells with varying dimensions. | Small and medium pouch cells with moderate variation in length and width. | Repeated production formats requiring stored recipes and accurate positioning. | Stable, standardized formats with high annual volumes and controlled upstream tolerances. |
| Typical cell-size range | Small laboratory cells up to approximately 300 × 200 mm, subject to fixture design. | Approximately 100–400 mm in length and 60–250 mm in width. | Approximately 150–600 mm in length and 80–350 mm in width. | Commonly configured for approximately 200–800 mm in length and 100–450 mm in width. |
| Positioning repeatability | Typically about ±0.5–1.0 mm, mainly dependent on the operator and fixture. | Typically about ±0.2–0.5 mm with a dedicated locating fixture. | Typically about ±0.05–0.20 mm using servo axes, sensors, and controlled clamping. | Typically about ±0.05–0.15 mm when upstream web and cell positioning are stable. |
| Typical trim-width control | Approximately ±0.5–1.0 mm. | Approximately ±0.3–0.5 mm. | Approximately ±0.1–0.3 mm. | Approximately ±0.1–0.2 mm with closed-loop alignment and maintained tooling. |
| Cutting method | Hand-operated guillotine, punch, or guided blade fixture. | Pneumatic or electric blade, punch, or shear activated after manual loading. | Servo-driven rotary knife, shear blade, or programmable punch with controlled motion. | Integrated rotary knife, die-cutting, or continuous shear system synchronized with line speed. |
| Material compatibility | Aluminum-plastic laminate pouch film and sealed edge areas; blade selection is application-specific. | Aluminum-plastic laminate with common sealant layers such as PP or PE-based structures. | Multilayer pouch films with different thicknesses, provided the tool pressure and blade geometry are qualified. | High-volume pouch-film structures requiring validated tooling, dust control, and continuous scrap removal. |
| Format changeover | Usually 5–15 minutes with interchangeable fixtures and manual adjustment. | Usually 10–30 minutes, depending on fixture and blade replacement requirements. | Usually 5–20 minutes with stored recipes and quick-change tooling. | Usually 15–45 minutes because tooling, conveyors, sensors, and line parameters may require coordinated setup. |
| Scrap handling | Manual removal and collection. | Basic chute or collection tray; manual emptying is common. | Powered scrap conveyor or vacuum extraction with bin-full detection. | Continuous scrap conveying or vacuum extraction with centralized collection and monitoring. |
| Quality-control capability | Visual inspection and manual measurement. | Basic presence sensors and optional dimensional checks. | Recipe verification, barcode or QR-code reading, edge-position detection, and optional vision inspection. | Integrated vision inspection, traceability, reject handling, process data collection, and line-level statistical monitoring. |
| Recommended controls | Simple electrical controls with guarded cutting area. | PLC control, two-hand start or light curtain, and emergency-stop circuit. | PLC with servo motion control, HMI recipes, safety doors, light curtains, and interlocked tooling. | Line PLC or industrial network communication, safety-rated motion control, access guarding, and MES-compatible data exchange. |
| Approximate equipment footprint | About 0.5–1.5 m². | About 1.5–4 m². | About 3–8 m², excluding external material handling. | About 8–25 m², depending on conveyors, feeders, inspection, and scrap systems. |
| Utility requirements | Electrical power; compressed air may not be required. | Electrical power and commonly 0.5–0.7 MPa compressed air for clamping or actuation. | Electrical power, compressed air, and optional vacuum extraction or dust collection. | Electrical power, compressed air, vacuum or dust extraction, network connection, and coordinated line utilities. |
| Main advantages | Lowest initial cost, simple operation, and maximum flexibility for development work. | Improved consistency and productivity without the complexity of a fully automated line. | High repeatability, recipe management, reduced labor, and strong adaptability to multiple formats. | Highest productivity, labor efficiency, traceability, and consistent integration with mass production. |
| Main limitations | Low throughput, operator-dependent quality, and limited process data. | Higher labor requirement and lower line efficiency than fully automatic equipment. | Higher investment, greater controls complexity, and need for trained maintenance personnel. | Highest capital cost, longer commissioning, stricter upstream quality requirements, and more complex maintenance. |
| Best choice when | Annual volume is low, cell designs are changing frequently, or the machine is mainly for R&D. | Production is growing and consistent trimming is needed, but full automation is not yet justified. | Multiple qualified formats must be produced with stable quality and medium-to-high utilization. | Demand is high, product formats are stable, and the trimming process must operate as part of an automated line. |
| Key questions before purchase | What is the largest cell, required edge geometry, and acceptable operator-dependent tolerance? | How many formats are required, and how frequently will fixtures or blades be changed? | What are the target takt time, trim tolerance, traceability requirements, and future format plans? | What are the line takt time, upstream and downstream interfaces, uptime target, reject strategy, and data-integration requirements? |
| Engineering note: The figures shown are typical planning ranges for pouch-cell trimming equipment and are not universal specifications. Final performance depends on pouch-film construction, sealed-edge thickness, cell dimensions, trim geometry, blade design, fixture accuracy, automation level, and the required acceptance criteria. Validate cutting quality, burrs, seal damage, particulate generation, and dimensional capability using representative production samples before final selection. | ||||